In construction and demolition (C&D) recycling operations, the ability to efficiently separate and sort mixed debris into usable aggregates is critical for both profitability and environmental compliance. Mobile vibrating screens have emerged as essential equipment on job sites where traditional fixed screening plants are impractical. These self-contained units offer flexibility, rapid deployment, and high throughput—making them indispensable for contractors and recyclers who need to process varying volumes of material at different locations. Understanding the technical parameters and operational benefits of mobile vibrating screens is the first step toward selecting the right solution for your recycling operation.

Why Mobile Vibrating Screens Are Essential for C&D Recycling

C&D waste typically contains concrete, asphalt, wood, metals, plastics, and soil—materials that require precise classification to recover value. Mobile vibrating screens are designed to handle this heterogeneous feed with minimal setup time. Unlike stationary systems, mobile units can be moved directly to the demolition site or stockpile, reducing transportation costs and eliminating the need for permanent infrastructure. Their ability to perform primary, secondary, or even tertiary screening in a single pass makes them versatile tools for producing multiple product fractions such as 0–5mm fines, 5–20mm aggregates, and oversized rejects.

Key Performance Factors in Mobile Vibrating Screens
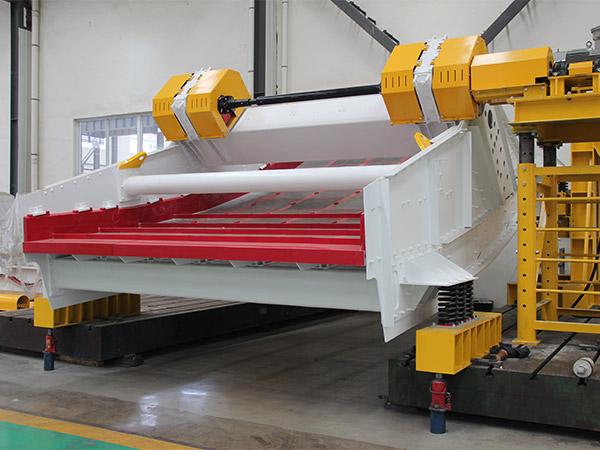
Linear Vibrating Screen

Vibration Mechanism and Stroke

The screening efficiency depends heavily on the vibration pattern—linear or circular motion. For sticky or wet C&D materials, circular motion with adjustable amplitude helps avoid blinding. Mobile screens from Haiside utilize a robust eccentric shaft design that delivers consistent stroke under heavy loads.

Deck Configuration and Surface Area

A larger screening area directly correlates to higher throughput. Standard mobile units offer double- or triple-deck configurations. Operators must balance the desired number of fractions against the machine’s overall transport dimensions. Haiside models incorporate quick-change screen panels to reduce downtime when switching between applications.

Mobility and Setup Efficiency

Time is money on active demolition sites. Hydraulic folding hoppers, track-mounted chassis, and wireless remote controls allow one operator to set up the plant in minutes. Many Haiside mobile screens feature a durable crawler undercarriage with high ground clearance for navigating rough terrain.

Advantages of Haiside Mobile Vibrating Screens Over Conventional Models

Haiside has engineered its mobile screening range with feedback from hundreds of recycling professionals. The following advantages set them apart:

  • High-frequency vibrating mechanism that prevents pegging and clogging even with moist demolition debris.
  • Integrated overband magnet available as a factory option to remove ferrous metals before screening.
  • Intelligent control system that monitors belt speed, vibration frequency, and engine load, adjusting parameters automatically for consistent quality.
  • Modular design allowing the main screenbox to be swapped between different sized decks in under two hours.
  • Compliance with European Stage V and EPA Tier 4 final emission standards, making them suitable for both urban and remote sites.

Selecting the Right Mobile Vibrating Screen for Your Application
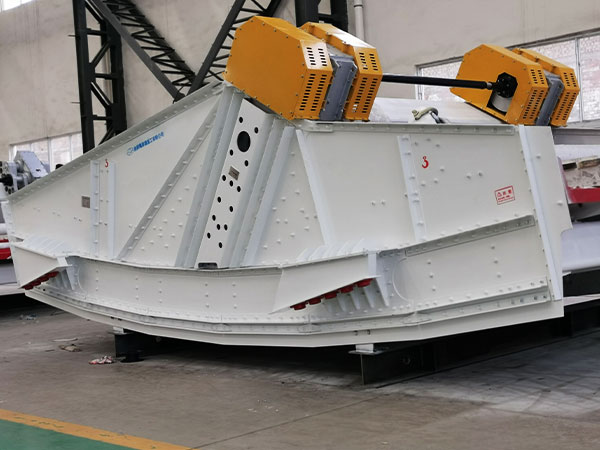
Every recycling operation has unique constraints. Consider these criteria before making a purchase decision:

…

For more details on mobile vibrating screens used in construction and demolition recycling, please click here: https://www.hsd-industry.com/news/mobile-vibrating-screens-for-construction-and-demolition-recycling/
Selecting the right screen media for vibrating equipment is a critical decision that directly impacts processing efficiency, product quality, and operating costs. Two of the most widely used materials—metal and polyurethane—offer distinctly different characteristics, and choosing between them requires a clear understanding of their performance under real-world conditions. This article provides an objective, technical comparison of metal and polyurethane screens, covering wear life, screening accuracy, operational considerations, and total cost of ownership. For operations seeking reliable, application-matched solutions, Haiside supplies both types of screen panels, enabling customers to make data-informed choices based on their specific material properties and production goals.

Overview of Metal Screens and Polyurethane Screens

Metal Screens: Construction and Typical Applications

Metal screens are manufactured from woven wire cloth or perforated metal plates. Common materials include high-carbon steel, stainless steel, and spring steel. Their open structure provides a high percentage of open area (typically 40–60%), which facilitates high throughput and efficient fines removal. Metal screens are widely used in mining, quarrying, and aggregate processing for coarse to medium screening where impact resistance and rapid material movement are priorities. However, they are susceptible to abrasion, corrosion in wet environments, and fatigue failure under heavy loads.

Polyurethane Screens: Composition and Key Characteristics

Polyurethane screens are made from cast or molded polyurethane elastomers, often reinforced with steel inserts for structural integrity. They offer superior resistance to abrasion and corrosion compared to metal, and their flexible nature reduces blinding and pegging in sticky or moist materials. The open area is lower (typically 30–45%) due to thicker cross-sections, but the material’s wear life can be 3 to 5 times longer than metal in abrasive conditions. Polyurethane panels are quieter in operation and lighter in weight, reducing dynamic loads on the vibrating equipment.

Key Performance Comparison

When evaluating these two screen types, several performance parameters must be weighed against each other. The following list highlights the most critical differences:

  • Wear Resistance: Polyurethane generally outlasts metal by a factor of 3–5 in abrasive applications. Metal screens wear more quickly, especially at wire intersections and along perforation edges.
  • Screening Efficiency: Metal screens typically offer higher open area, leading to greater throughput. Polyurethane’s flexibility can actually improve stratification and reduce near-size particle retention, but reduced open area may lower capacity.
  • Blinding and Peeling: Polyurethane is less prone to blinding because of its non-stick surface and ability to flex. Metal screens tend to clog with moist or clay-rich materials.
  • Noise and Vibration: Polyurethane dampens noise by 5–10 dB compared to metal, creating a quieter working environment. It also transmits less vibration to the support structure.
  • Weight: Polyurethane panels are significantly lighter, reducing startup torque and wear on bearings and frames.
  • Temperature Tolerance: Metal screens can withstand temperatures up to 400°C (depending on alloy), while polyurethane is typically limited to 80–90°C.

Long-Term Cost Analysis (Total Cost of Ownership)

Initial purchase price often favors metal screens, which can be 30–60% less expensive per panel than equivalent polyurethane. However, total cost of ownership (TCO) must account for replacement frequency, downtime losses, and maintenance labor. In high-abrasion environments (e.g., iron ore, copper, crushed granite), a single polyurethane panel may replace three to five metal panels over its life. Reduced changeover downtime and lower inventory requirements can further tilt the balance. For wet screening operations where corrosion accelerates metal degradation, polyurethane offers even greater economic advantage. Haiside provides detailed TCO estimates to help operators compare scenarios specific to their throughput and material characteristics.

…

For more detailed information comparing metal screens and polyurethane screens used in vibrating equipment, please click here: https://www.hsd-industry.com/news/comparing-metal-and-polyurethane-screens-for-vibrating-equipment/

Factories generate significant volumes of scrap metal, wood chips, or biomass every day. Hauling this waste off-site is expensive, and the logistical hassle often interrupts production flow. A mobile briquetting unit brings the compaction process directly to the waste source, converting loose material into dense, saleable briquettes within your facility. This article examines the technology behind mobile briquetting, its key advantages over stationary systems, and how ZYmining’s solution can help your factory turn a disposal cost into a revenue stream.

The Growing Need for On-Site Waste Processing

Environmental regulations and rising landfill fees have forced manufacturers to rethink waste management. Traditional methods—storing scrap in bins, hiring trucks, and paying per ton for disposal—are no longer cost-effective or sustainable. On-site processing not only reduces transportation costs but also cuts carbon emissions associated with hauling.

Traditional waste management challenges

  • High logistics cost: Frequent pickups by third-party haulers eat into profit margins.
  • Space inefficiency: Loose scrap occupies large floor areas, reducing usable factory space.
  • Safety hazards: Piles of sharp or dusty waste increase workplace accident risks.
  • Lost opportunity: Many waste materials have intrinsic value if properly compacted and sold.

A mobile briquetting unit directly addresses each of these pain points by enabling immediate, controlled compaction at the point of generation.

What Is a Mobile Briquetting Unit and How Does It Work?

mobile briquetting unit

A mobile briquetting unit is a compact, wheeled or trailer-mounted machine that uses hydraulic pressure to compress loose material into uniform briquettes. Unlike fixed industrial presses that require concrete foundations and permanent installation, a mobile unit can be moved between production lines, warehouses, or even different factory sites.

The process is straightforward: waste material is fed into a hopper, conveyed to a compression chamber, and then extruded through a die under high pressure (typically 100-200 bar). The resulting briquettes are dense, low‑moisture, and easy to stack or transport. ZYmining’s mobile briquetting units are engineered for continuous operation with minimal maintenance, featuring durable hydraulic systems and automated controls.

Key Advantages of ZYmining’s Mobile Briquetting Unit

When comparing mobile briquetting to fixed installations, several decisive benefits emerge:

Mobile vs. Stationary Briquetting Systems

  • Installation & setup: Mobile unit – no foundation needed, plug-and-play in hours. Stationary – requires civil engineering, concrete pad, and days of installation.
  • Flexibility: Mobile unit – can be relocated to follow production changes or moved between facilities. Stationary – permanently fixed, limiting reconfiguration.
  • Capital investment: Mobile unit – lower initial cost, often 30–40% less than equivalent stationary press. Stationary – higher upfront expenditure.
  • Maintenance access: Mobile unit – all components accessible; maintenance can be performed without disrupting factory layout. Stationary – may require special crane access or partial disassembly.
  • Scalability: Mobile unit – add multiple units as waste volume grows. Stationary – capacity is fixed at installation.
  • Resale value: Mobile unit – retains higher resale due to portability. Stationary – low resale because removal is costly.

…

For more details on mobile briquetting equipment—designed for processing waste materials directly at your factory site—please click here: https://www.zymining.com/en/a/news/mobile-briquetting-unit.html

Grinding circuits can consume more than half of a mineral processing plant’s total electrical load, so the choice between high-pressure grinding rolls (HPGR) and conventional ball mills is rarely a purely technical preference — it is a cost decision. Both routes reduce ore to a comparable target size, but they achieve it through fundamentally different breakage mechanisms, and that difference shows up directly in kWh per tonne. This comparison examines where the energy actually goes, what typical specific energy values look like in each route, and under which conditions one technology delivers a genuinely lower power bill for your circuit.

Why Comminution Energy Is So Hard to Reduce

Crushing and grinding are thermodynamically inefficient by nature. Estimates in the technical literature commonly place the energy that actually creates new fracture surface at well under 5% of the total power drawn by a mill. The remainder is lost to elastic deformation, inter-particle friction, heat, noise, and vibration. That single fact explains why the industry keeps searching for a more efficient breakage mechanism rather than simply building larger drives.

Energy consumption in comminution scales with the reduction ratio and the ore’s resistance to breakage, usually expressed through the Bond work index (Wi) or a more recent hardness parameter. Two levers therefore exist: reduce the amount of size reduction work required, or change the way the force is applied so that more of it reaches the particle rather than the machine. HPGR and ball mills differ most sharply on the second lever.

HPGR vs Ball Mill: Two Different Breakage Mechanisms

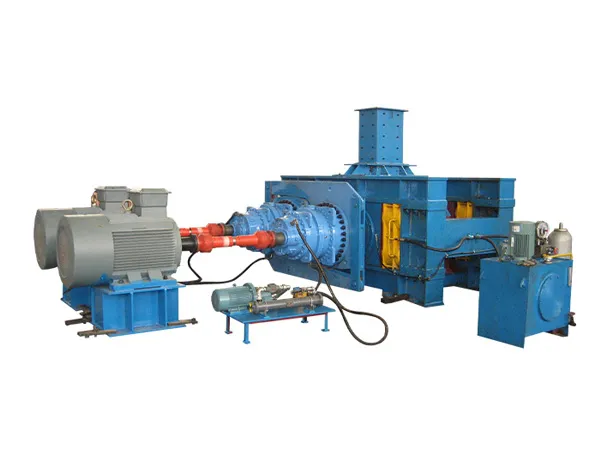
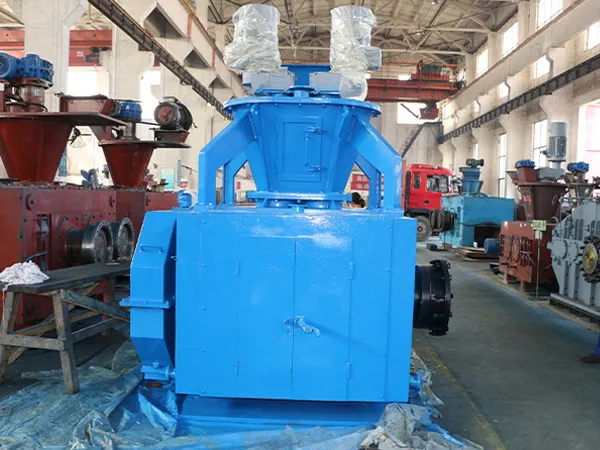
high-pressure grinding rolls

How a ball mill breaks rock

A ball mill is a tumbling cylinder filled with steel media. As the shell rotates, the charge is lifted and then cascades or cataracts, delivering a mix of impact and attrition to the ore. Breakage is largely random and single-particle in nature: a grinding ball strikes a particle, or particles are abraded between media. Unavoidable energy sinks include lifting the entire media charge, grinding the liners and media themselves, and producing fines that were already liberated. Slurry transport and classification inside the mill also absorb power.

How HPGR breaks rock

HPGR forces a packed bed of particles between two counter-rotating rolls at very high pressure. Breakage occurs through inter-particle compression: particles press against each other, so the applied force is distributed across many contact points rather than concentrated on a single impact. The result is a product with a high proportion of fines and, critically, a network of micro-cracks along grain boundaries. Those micro-cracks weaken the material for downstream grinding, which is where a large part of the real energy saving originates.

Energy Consumption Compared: What the Numbers Look Like

Exact values depend heavily on ore hardness and target size, but published plant data and vendor test work generally fall into recognizable bands:

  • HPGR stage (tertiary crushing duty): typically in the range of 1.5 to 3.5 kWh per tonne of fresh feed, depending on roll pressure and circulating load.
  • Ball mill stage (fine grinding to roughly 75 to 100 microns): commonly 10 to 25 kWh per tonne, driven mainly by Bond work index and the reduction ratio.
  • Combined HPGR plus ball mill circuit: total grinding energy is frequently reported to be 15% to 30% lower than an equivalent conventional crush-and-ball-mill circuit producing the same product size.

…

For more detailed information on high-pressure grinding rolls (HPGR) versus ball mills—and which offers the best energy-saving performance—please click here: https://www.zymining.com/en/a/news/hpgr-vs-ball-mill.html

Comminution is the largest single consumer of electrical energy in most mineral processing plants, and in hard-rock operations it can account for the majority of the site’s power draw. Every kilowatt-hour removed from the grinding circuit therefore flows straight to the bottom line. High-pressure grinding rolls, commonly known as HPGR, have become one of the most credible ways to achieve that reduction, not because they grind more aggressively, but because they break ore in a fundamentally different way. This article explains the mechanism behind HPGR power savings, identifies exactly where the energy gains originate, and sets out the design and operating factors that determine whether those savings are realised in practice rather than simply promised on a datasheet.

Why Conventional Grinding Circuits Consume So Much Power

Tumbling mills, whether autogenous, semi-autogenous or ball mills, break rock through a combination of impact and abrasion inside a rotating shell. The problem is one of energy transfer efficiency. A significant share of the electrical energy delivered to the mill motor is dissipated as heat, noise, vibration and steel media wear rather than as new fracture surface. Lifting the charge, rotating the shell and the mill’s own drivetrain all absorb power before any rock is broken at all.

Two further inefficiencies compound the problem. First, tumbling mills tend to over-grind a portion of the feed while under-grinding the coarsest particles, because residence time is distributed unevenly. Second, liberation is achieved by grinding everything finer than necessary, which consumes energy on material that is already sufficiently liberated. The core inefficiency of conventional grinding is that energy is applied to a random charge rather than directly to the particles that need breaking.

How High-Pressure Grinding Rolls Break Rock Differently

High-Pressure Grinding Rolls

HPGR operates on a principle known as inter-particle, or bed, comminution. Material is fed between two counter-rotating rolls, one of which is fixed while the other is held under hydraulic pressure. The gap is deliberately choked with material, so particles are compressed against one another rather than crushed between two steel surfaces.

Inter-particle compression

As the feed enters the compression zone, roll pressure builds to several tens of megapascals and the particle bed is compacted into a dense cake, often called a flake or scurf. Individual particles are loaded from multiple directions by their neighbours. Because the load is distributed across the whole bed, breakage occurs throughout the material rather than only at the surfaces of the rolls, and the energy is applied to the ore instead of to grinding media.

Micro-cracking and weakened product

The most commercially valuable outcome of HPGR is not the immediate size reduction but the damage left behind. Compression along grain boundaries generates a network of micro-cracks through each particle. The discharge cake looks coarse, yet the particles are structurally weakened. When that material reports to a downstream ball mill or stirred mill, it fractures far more easily, which reduces the specific energy required in the following stage. This is the mechanism by which HPGR savings extend well beyond the rolls themselves.

Where the Power Savings Actually Come From

It is worth being precise about the sources of savings, because they are often presented as a single headline figure. In reality the gain is the sum of several distinct effects:

  • Direct energy application: compressive force is transferred to the particle bed through a short, efficient hydraulic and mechanical path, with no need to lift a grinding charge against gravity.
  • No grinding media: the process eliminates steel ball or rod consumption, removing both the embodied energy of media production and the power previously lost to media-to-media collisions.
  • Micro-crack pre-conditioning: weakened product lowers the Bond work index of the downstream mill feed, cutting specific energy in the secondary grinding stage.
  • Reduced over-grinding: the narrow compression zone limits residence time, so fewer fines are produced unnecessarily.

…

For more details on how high-pressure grinding rolls (HPGR) can save electricity, please click here: https://www.zymining.com/en/a/news/hpgr-power-savings.html

High Pressure Grinding Rolls (HPGR) are among the most efficient comminution devices in modern mineral processing, but their performance hinges on the condition of the roll surface. When wear takes hold, throughput drops, energy consumption climbs, and product size distribution becomes unpredictable. For plant managers and maintenance engineers, understanding why HPGR rolls wear and how to fix it is not just a technical concern—it directly affects operational cost and circuit stability. This article breaks down the root causes of HPGR roll wear and outlines practical fixes that restore performance and extend service life.

Why HPGR Roll Wear Deserves Immediate Attention

Unlike conventional crushing equipment, HPGR relies on inter-particle comminution. Ore is compressed between two counter-rotating rolls under extreme pressure, causing particles to fracture against one another. This process minimizes energy waste, but it also subjects the roll surface to relentless abrasive and fatigue loading. A worn roll surface alters the nip angle, reduces the effective pressure transfer, and can lead to a cascade of downstream issues—including poor liberation, increased circulating loads, and higher wear rates in subsequent grinding stages.

The economic impact is substantial. Unplanned roll changes can halt production for hours or even days, and premature roll replacement adds directly to consumable costs. Detecting wear early and addressing its root cause is far cheaper than reacting to a catastrophic failure.

Root Causes of HPGR Roll Wear

Abrasive and Hard Ore Characteristics

The single largest driver of roll wear is the abrasiveness of the feed material. Ores with high silica content, hard quartz, or sharp, angular particles act like a grinding wheel against the roll surface. The wear mechanism is primarily three-body abrasion: ore particles trapped between the roll and the feed create localized scratching and gouging. Over time, this erodes the hardfacing or studded surface, reducing the roll’s ability to grip and compress the material bed.

High Cyclic Stress and Fatigue

Every rotation of the roll subjects the surface to repeated compressive stress cycles. In high-throughput operations, a single roll can endure millions of loading cycles per month. This cyclic loading leads to subsurface fatigue cracking, particularly in areas where the hardfacing has imperfect bonding or where the base material lacks sufficient toughness. Once cracks initiate, they propagate under continued loading, eventually causing spalling or chunk detachment.

Thermal Effects and Heat Build-Up

HPGR operates with a significant amount of friction between the rolls and the material bed. While some heat is expected, inadequate cooling or excessive roll speed can cause localized overheating. Thermal expansion and contraction cycles weaken the bond between the hardfacing and the roll body. In extreme cases, thermal cracking accelerates wear and leads to premature roll failure.

Improper Operating Parameters

  • Excessive roll speed: increases sliding abrasion and reduces the formation of a stable material bed.
  • Incorrect nip pressure: too low a pressure prevents inter-particle comminution; too high a pressure overloads the surface.
  • Uneven feed distribution: creates localized wear zones and skews the roll profile.
  • Moisture imbalance: wet or sticky feed can cause slip and abnormal wear patterns.

Identifying HPGR Roll Wear Patterns

…

For more detailed information on roller wear in high-pressure grinding rolls (HPGR)—including causes and solutions—please click here: https://www.zymining.com/en/a/news/hpgr-roll-wear.html

As wind turbine towers evolve toward taller, more efficient designs, manufacturers increasingly encounter non-round tower sections—elliptical, polygonal, or tapered geometries that challenge conventional round clamping methods. Standard lathe chucks fail to grip these irregular profiles securely, leading to vibration, dimensional inaccuracies, and increased scrap rates. Customizable chuck systems have become a critical solution, enabling precise workholding for complex tower segment geometries. This article examines how BOTA’s engineered chuck systems address the unique demands of non-round wind tower sections, providing superior rigidity, adaptability, and process repeatability.

Why Non-Round Tower Sections Demand Specialized Chuck Systems

Modern wind tower designs often incorporate non-round cross-sections to optimize material usage, reduce wind loads, or accommodate internal components. Common examples include:

  • Elliptical sections that reduce drag and improve structural efficiency
  • Polygonal (hexagonal/octagonal) sections for easier assembly or increased rigidity
  • Tapered sections with variable diameter along the length
  • Hybrid profiles combining flat and curved walls

Standard three- or four-jaw chucks designed for cylindrical parts cannot provide uniform clamping force across these non-round surfaces. The result is often workpiece slippage, eccentric rotation, or stress concentrations that deform the part. Customizable chuck systems are engineered to match the exact contour of each section, distributing clamping forces evenly and maintaining workpiece stability during machining operations.

Clamping Force Distribution in Irregular Geometries

The fundamental challenge lies in the geometry of force application. On a round surface, a three-jaw chuck naturally centers the part. On a non-round profile, the contact points must be designed to avoid point loads that could bend thin-walled tower sections. BOTA’s approach uses modular jaw inserts that conform to the section’s curvature, combined with synchronized actuation to ensure balanced gripping without distortion.

Key Features of BOTA’s Customizable Chuck Systems

Wind Tower Welding Rotator

BOTA has developed a family of chuck systems specifically for non-round wind tower sections. These systems are built around a modular base that accepts interchangeable jaw carriers, enabling rapid changeover between different profile geometries. Critical features include:

1. Adaptive Jaw Profiles

Each jaw face is machined from high-strength alloy steel to match the customer’s specific section profile—whether elliptical, polygonal, or compound curve. The jaws incorporate replaceable hardened pads that can be swapped when worn or when a new profile is required. This approach reduces tooling costs and lead times for prototype or low-volume runs.

2. Hydraulic or Mechanical Actuation Options

BOTA offers both hydraulic and mechanical actuation depending on the production environment. Hydraulic systems provide consistent clamping force automatically, ideal for high-volume automated cells. Mechanical systems (manual or power-torqued) suit job-shop environments where flexibility outweighs automation. Both options include integrated safety interlocks that prevent spindle rotation if insufficient clamping pressure is detected.

…

For more details on customizable chuck systems suitable for non-circular wind tower sections, please click here: https://www.bota-weld.com/en/a/news/chuck-systems-non-round.html

In the competitive landscape of wind energy construction, every minute of assembly time directly impacts project profitability. Traditional methods for rotating tower sections – cranes, manual rigging, or hydraulic jacks – often introduce bottlenecks that stretch cycle times well beyond optimal. BOTA’s field-proven wind tower rotator redefines this process, delivering a consistent 30% faster cycle time in real-world conditions. This article examines the engineering behind that claim, the measurable field results, and why project managers are switching to this solution for onshore and offshore installations.

Understanding the Value of Cycle Time in Tower Erection

Cycle time – the duration from initial pick-up of a tower section to its secure positioning and bolt-up – is a critical operational metric. Even modest reductions compound across dozens of towers per project. A 30% faster cycle time translates into:

  • Fewer crane hours and lower rental costs.
  • Shorter per-tower installation windows, enabling more turbines per weather window.
  • Reduced labor fatigue and improved safety through fewer manual adjustments.

BOTA’s rotator directly addresses the most time-consuming step: aligning and rotating the heavy steel sections before hoisting. By automating this with a controlled, high-torque rotation system, the rotator eliminates the need for tag lines, multiple crane lifts, or time-consuming re-rigging.

Engineering Breakthrough: How BOTA Achieves 30% Faster Cycle Time

Wind Tower Welding Rotator

The BOTA wind tower rotator combines three core innovations:

Hydraulic Direct-Drive Rotation

Unlike gear-driven designs that require high maintenance and slower start/stop, BOTA uses a direct-drive hydraulic motor that delivers instant full torque from zero RPM. The result is smooth, precise rotation without the backlash that slows down conventional systems.

Adaptive Clamping Mechanism

The rotator’s self-centering clamps adjust to varying tower diameters (3–5 meters) in under 30 seconds. This eliminates the need for custom fitments or manual shimming, a common source of delays on the field.

Integrated Inclinometer and Control Logic

Operators can pre-program rotation angles (0–360°) with ±0.5° accuracy. The system’s inclinometer continuously monitors tilt, automatically compensating for uneven ground or wind gusts. This reduces the need for spotter communication and re-positioning attempts.

Field tests by BOTA recorded an average rotation + alignment time of 4 minutes 20 seconds per section, compared to 6 minutes 12 seconds with traditional tag-line methods – a 30.1% reduction.

Field-Proven Performance: Real Project Data

BOTA deployed the wind tower rotator across three wind farms in Q2–Q3 2024. Cumulative data from 87 towers shows:

  • Average cycle time (pick-up to bolt-up): 7.8 minutes per section.
  • Average reduction vs. baseline (traditional method): 30.2%.
  • Zero safety incidents related to rotation or alignment.
  • Operators reported a learning curve of less than 2 hours.

…

For more details on how a wind tower rotator—proven in the field—can reduce cycle times by 30%, please click here: https://www.bota-weld.com/en/a/news/wind-tower-rotator-delivers-faster-cycle-time.html

Welding rotators look simple from a distance: two sets of wheels, a frame, a drive. Yet the specification sheet behind them decides whether a fabrication shop produces consistent circumferential welds or spends its days chasing arc wander and rework. Buyers who treat capacity, rotation speed, and control as three independent checkboxes often end up with a machine that either stalls under a heavy vessel or turns too fast for a delicate root pass. The three variables are interdependent — load determines wheel loading, wheel loading constrains available torque, and torque sets the usable speed range under control. This guide walks through each specification in the order a buyer should evaluate it, with the practical checks that separate a rotator that runs for fifteen years from one that disappoints in six months.

Capacity: The Specification That Governs Everything Else

Capacity is quoted as a single tonnage figure, which makes it the easiest spec to compare and the easiest to misread. That figure normally assumes the workpiece center of gravity sits close to the rotational axis, with the load shared evenly between the two wheel sets. Real vessels rarely cooperate.

Rated Load vs. Real-World Load

A shell with a heavy nozzle cluster, an offset manway, or internal baffles shifts the center of gravity away from the axis, and the load on one wheel set rises while the other drops. For eccentric or asymmetric workpieces, effective wheel loading can exceed the nominal figure by 15 to 25 percent. Rather than applying a blanket derating factor, send the supplier your actual part drawing and ask for a wheel-load calculation. A reputable manufacturer will run that number before quoting, not after the machine is on your floor.

Also confirm whether the rating applies to the rotating load alone or includes tooling, fixturing, and a welding head mounted on the frame. Accessories add weight that the drive still has to turn.

Wheel Diameter, Wheel Type, and Vessel Geometry

Wheels are where capacity becomes physical. Three decisions matter:

  • Wheel material. Polyurethane wheels protect finished surfaces on stainless, aluminum, and painted vessels. Steel wheels handle hot workpieces and heavy carbon steel sections where surface marring is not a concern.
  • Wheel diameter. Larger wheels spread contact stress over more area, which reduces the risk of denting thin-wall shells and improves grip on polished surfaces.
  • Wheelbase adjustment. The distance between wheel sets determines the minimum and maximum vessel diameter a single unit can carry. A powered adjustable base costs more but pays for itself the moment you rotate a third or fourth diameter.

BOTA sizes wheel sets and wheelbases against part drawings rather than catalog ranges, because a rotator that technically fits a diameter but contacts the shell at the wrong angle will slip under load.

Rotation Speed: Matching Turn Rate to the Welding Process

Welding Rotator

Most circumferential welding falls somewhere between roughly 0.1 and 1.0 rpm, but the top speed on a datasheet tells you very little. The number that matters is the lowest stable speed the unit can hold under full load without stalling, surging, or cogging.

Variable Speed Is Not Optional

A fixed-speed rotator suits one repetitive job and nothing else. As soon as your workpiece diameter, wall thickness, or process changes, travel speed has to change with it. Three drive approaches dominate the market:

  • Mechanical variable speed (belt or disc): inexpensive and simple, but adjustment range is narrow and torque falls off at low speeds.
  • AC variable-frequency drive: the industry workhorse. Wide adjustment range, dependable torque at low rpm, and straightforward maintenance.
  • Servo or closed-loop DC: the tightest speed regulation, best for automated cells where the rotator must track a welding program.

Torque and Turn-Down Ratio

Ask for a torque curve, not just a horsepower rating. A drive that turns 5 rpm freely may stall at 0.2 rpm with a 20-ton vessel on the wheels. Look at the turn-down ratio — the span between maximum and minimum controllable speed — and confirm that the low end is rated at full load. If the answer is vague, the low-speed performance probably is too.

…

For more detailed information on selecting welding rotators—covering capacity, speed, and controls—please click here: https://www.bota-weld.com/en/a/news/welding-rotator-buying-guide.html

Selecting a welding rotator for heavy pipe fabrication is a capacity and safety decision, not a catalog exercise. A rotator that is undersized for a large-diameter spool will slip, vibrate, and pull the weld seam out of position; one that is oversized wastes floor space, power, and capital. The variables that matter most are the actual load carried by each wheel, the pipe diameter range you plan to run, the drive configuration, and how precisely rotation speed must match your welding process. This guide follows the specification decisions in the order most fabrication shops make them, from load calculation through control system selection, and explains where a supplier’s engineering support makes a measurable difference to throughput and weld quality.

Calculate the True Load Before Comparing Models

Catalog capacity ratings describe a balanced, static load. Real pipe fabrication rarely looks like that. Before you compare models, work out what each rotator will actually carry during the heaviest job you expect to run.

Dead Weight, Tooling and Dynamic Load

  • Pipe dead weight — the bare spool or pipe section, including wall thickness, flanges, and end caps.
  • Fittings and attachments — branch connections, elbows, and pre-welded nozzles shift the center of gravity and create eccentric loading.
  • Internal components — liners, internal sleeves, or water used for hydro testing add substantial mass.
  • Weld tooling — positioners, alignment clamps, and spider assemblies ride on the pipe and must be included.
  • Dynamic effects — starting torque, braking, and any imbalance during rotation generate forces higher than the static weight.

A practical rule: calculate the worst-case total, then apply a working safety margin instead of buying exactly at the rated figure. Where a long pipe spans two rotators, remember the load is not split evenly — an off-center fitting can push most of the weight onto one unit. If you cannot confidently determine the distribution, ask the supplier to review the pipe drawing rather than guessing.

Duty Cycle and Continuous Operation

A rotator used for occasional fit-up and tacking has different requirements from one running continuously under a submerged arc or narrow-gap welding head. Continuous rotation at low speed for hours heats the motor and gearbox, and it demands a drive rated for that duty cycle. State your expected hours per shift and whether the rotator will run unattended for long welds.

Match the Rotator to Your Pipe Diameter Range

Capacity is only half the specification. Diameter range determines wheel spacing, frame geometry, and whether the rotator is adjustable at all.

  • Fixed-center (conventional) rotators hold one wheel spacing and suit a narrow, repeating product range.
  • Adjustable / bolt-on rotators allow wheel positions to be repositioned for different diameters — useful for job shops.
  • Self-aligning (self-centering) rotators automatically adjust to the pipe, which shortens changeover time and improves repeatability.

Two details cause most problems. First, running small-diameter pipe on a rotator sized for large diameters raises the pipe too high and can cause the wheels to lose contact under load. Second, rotation speed for welding is normally set as surface speed, not RPM — a small pipe and a large pipe at the same RPM rotate at very different linear speeds. Confirm the rotator’s speed range covers the surface speed your welding procedure requires at both ends of your diameter range.

Choose the Right Drive Configuration

The drive arrangement determines torque, tracking, and how easily the pipe stays aligned with the weld head.

  • Single powered rotator with an idler — cost-effective for lighter loads and shorter pipe; the idler follows rotation passively.
  • Dual powered rotators — both units are driven and synchronized, which is the usual choice for heavy wall pipe and long spools where torque demand and slip risk are high.
  • AC motor with variable frequency drive — the most common configuration; provides smooth, stepless speed control and good low-speed torque.
  • DC or hydraulic drive — considered where very high torque, harsh environments, or existing plant power infrastructure favor them.

For heavy pipe fabrication, dual-drive synchronous rotation is rarely optional. Mismatched rotation between a powered rotator and a passive idler introduces torsional stress and drift that shows up as inconsistent penetration and bead appearance.

Wheel Material, Hardness and Surface Protection

Wheel selection affects grip, marking, and pipe finish. Polyurethane wheels protect stainless, aluminum, and coated pipe from contamination and surface damage. Steel wheels handle the heaviest loads and high temperatures but can mark softer material. Rubber or composite wheels sit between the two and suit general carbon steel work. Check wheel diameter as well: larger wheels reduce contact pressure and roll more smoothly over longitudinal seams and weld caps, which matters when the pipe surface is not perfectly round.

…

For more details on how to select the right welding rotator for heavy-duty pipe fabrication, please click here: https://www.bota-weld.com/en/a/news/welding-rotator.html